
Table of Contents
- How Cutting Accuracy Drives Production Costs
- The Cost of Scrap in Manufacturing
- Material Yield Optimization and Precision
- Cutting Rework Reduction and Its Financial Impact
- Automated Cutting Systems and Cost Performance
- Measuring Accuracy: KPIs That Matter to Your Bottom Line
- Building Your Accuracy Improvement Workflow
- Frequently Asked Questions
Last Updated: October 5, 2026
How Cutting Accuracy Drives Production Costs
Cutting accuracy directly determines your total manufacturing cost, making it essential for cutting accuracy production costs. It’s not just about precise cuts, it’s what happens downstream: less waste, fewer defects, reduced rework, faster throughput. When your process drifts out of tolerance, the financial impact ripples through your entire operation.
Manufacturers who prioritize cutting accuracy see measurable gains in material yield, labor productivity, and profit margins. The relationship is quantifiable.
Here’s what most guides miss: cutting accuracy isn’t a metric you optimize in isolation. It’s a cost driver connected to every other production variable. Better accuracy reduces scrap, which improves material yield, the core of cutting accuracy production costs, which lowers per-unit cost.
The Cost of Scrap in Manufacturing
Scrap is pure financial loss: every piece of material that doesn’t reach a finished product is money spent with no return.
Scrap comes from three sources:
- Cutting errors, Inaccurate cuts produce parts outside tolerance
- Material defects, Flaws in incoming material that cutting can’t prevent
- Setup waste, Unavoidable trim and edge loss during nesting and cutting
Cutting accuracy directly controls the first category. Tight tolerances mean fewer parts fail inspection, so your scrap rate drops.
The financial impact scales with volume. A small operation losing 2% of material to cutting errors might absorb it; a mid-sized operation cutting 10,000 units per month can’t, that 2% becomes a six-figure annual loss.
Material waste also compounds: scrap ties up working capital, requires disposal, and often can’t be recovered. High-accuracy cutting systems reduce scrap at the source, lowering material costs per finished unit.
Material Yield Optimization and Precision
Material yield is the percentage of incoming material that becomes finished product. Everything else is waste.
Yield depends on three factors:
- Nesting efficiency, How well patterns fit on the material
- Cutting precision, How accurately cuts follow the pattern
- First-pass quality, How many parts pass inspection without rework
Cutting accuracy affects the second and third directly: precise cuts mean parts fit specifications, so they skip rework and move straight to assembly.
Poor cutting accuracy forces rework, which consumes labor, delays production, and often produces scrap when parts can’t be salvaged. The cost compounds: labor, material, time, and opportunity cost.
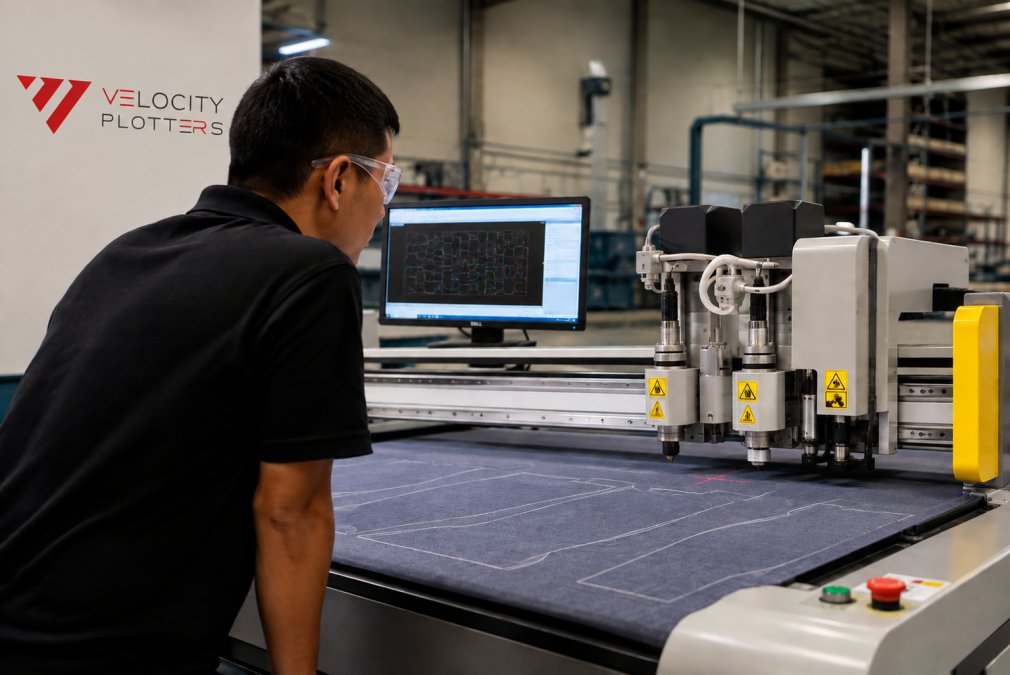
Precision tooling and machine setup determine cutting accuracy: dull blades, worn fixtures, and poor calibration all reduce it. Regular maintenance is foundational, and automated cutting systems like those from Velocity Plotters eliminate many setup variables, improving consistency and yield.
Cutting Rework Reduction and Its Financial Impact
Rework is the most expensive form of waste, consuming labor twice: once for the original cut, again to fix or replace the part.
When cutting accuracy is poor, rework becomes routine: operators spend hours per shift fixing undersized or oversized parts, and some become scrap. The labor cost is significant; the lost production time is worse.
Rework also creates bottlenecks. If cutting produces defects faster than rework can handle them, parts pile up. Production slows. Deadlines slip. Customers see delays.
Reducing rework starts with cutting accuracy: higher accuracy means fewer defects, less rework, and more time for productive cutting.
The financial benefit is direct: every hour on rework is an hour not spent cutting new parts. Improve accuracy, reduce rework, and you recover that labor capacity for revenue-generating work.
Automated Cutting Systems and Cost Performance
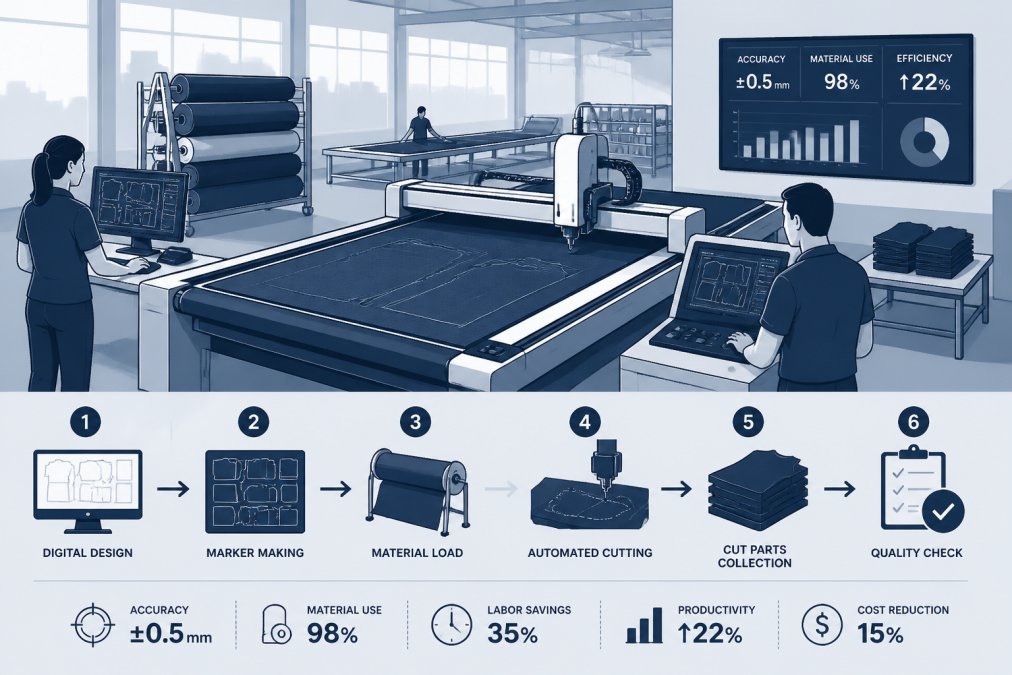
Automated cutting systems deliver accuracy manual cutting can’t match, plus consistency, which is equally important.
Manual cutting depends on operator skill, attention, and fatigue; even skilled operators produce variation. Automated systems follow programmed paths with precision, don’t get tired, and don’t drift out of tolerance over a shift.
The cost benefit compounds: in month one, automated systems reduce scrap and rework; by month three, throughput improves; by month six, labor productivity rises as operators spend less time on rework.
Automated systems also enable design for manufacturing: CAD-to-cutter software integration means design changes reach production without manual translation, eliminating a source of error.
Setup time also drops: manual systems require physical setup for each pattern change, while automated systems load software and run. Faster changeovers mean higher throughput and lower per-unit cost.
Measuring Accuracy: KPIs That Matter to Your Bottom Line
Most guides tell you to “track quality.” That’s not a KPI, it’s a wish. To connect cutting accuracy to production cost, you need metrics defined by a formula, tied to a dollar figure, and reviewed on a fixed cadence.
Dimensional deviation. The measured difference between the actual cut edge and the nominal print dimension.
Tolerance capability (Cpk). How well your process fits inside the print tolerance band.
First-pass yield (FPY). Parts that pass inspection without rework or scrap, divided by parts started. If you cut 1,000 parts and 940 pass clean, FPY is 94%. FPY is the multiplier that turns cutting accuracy into throughput.
Scrap rate. Material lost to cutting errors divided by material issued. Track it separately from setup waste and incoming-material defects, blending them hides the accuracy problem.
Rework rate. Parts requiring rework divided by parts inspected. Pair it with rework hours per shift so you can price the labor.
Cost per good unit. Total production cost (material + labor + machine time + inspection + rework + scrap) divided by good parts shipped. This is the only KPI that speaks the language of your P&L.
How the metrics roll up. The chain is simple arithmetic: cutting accuracy drives dimensional deviation, which drives Cpk, which drives FPY, which drives scrap and rework, which drive cost per good unit. Plot those six numbers on one weekly chart and accuracy becomes a cost line.
Cadence and sampling. Weekly review is the minimum; daily for high-volume operations. Sample the same way every time, same nest position, measurement points, and gauge, or your trend line is noise.
Tools. Manual calipers and tape measures are fine for spot checks but too slow and operator-dependent for trend data.
What good looks like. A stable cutting process often runs Cpk above 1.33, FPY above 95%, and scrap from cutting errors under 1% of material issued.
The diminishing-returns trap. Tighter tolerance isn’t free: every step adds machine time, inspection time, and tooling wear.
Building Your Accuracy Improvement Workflow
A workflow that says “check your blades” isn’t a workflow, it’s a checklist. The version below is diagnostic: each step tells you what to measure, what a bad reading looks like, and what it costs if you ignore it. It also ends with a worked per-part example so you can see how the numbers connect.
Step 1: Establish a cost baseline, not just a quality baseline. Before changing anything, calculate cost per good unit for the last four weeks: pull material issued, labor hours (cutting + rework + inspection), machine hours, and good parts shipped, then divide total cost by good parts. Every improvement is measured against that number.
Step 2: Rank the loss sources. Using your KPI data, sort losses into four buckets: scrap from cutting errors, rework labor, inspection labor, and machine time lost to re-cuts. Start with the largest.
Step 3: Run a five-point diagnostic. For each cutting station, check these in order:
- Machine calibration. Verify square, belt tension or rack-and-pinion backlash, and encoder zero. A drift of a few thousandths at the gantry can double at the far corner of a large nest.
- Tooling condition. Measure blade or bit wear against the manufacturer’s wear limit, not against “it still cuts.” A worn tool cuts a wider kerf, which changes both part dimension and material yield.
- Material variation. Check incoming thickness, moisture, and lot-to-lot dimensional consistency. Material that varies more than your tolerance band makes the tolerance unachievable no matter how good the machine is.
- Nesting and pattern placement. Verify that the nest software is using the actual kerf width, not a default. A 0.010-inch kerf error multiplied across hundreds of inches of cut path is real material.
- Operator setup. Confirm that origin, rotation, and material registration are set the same way on every shift. Setup variation is the most common hidden cause of “random” accuracy drift.
Step 4: Fix the largest driver first. If calibration is off, recalibrate and add a weekly verification cut. If tooling is worn, set a replacement schedule based on inches cut, not calendar days. If material varies, add an incoming inspection gate. Change one variable at a time, three at once tells you nothing about which worked.
Step 5: Re-measure after two weeks. Recalculate cost per good unit. If it dropped, the fix worked. If it didn’t, the loss was somewhere else, go back to Step 2 with fresh data.
Step 6: Standardize and scale. Write the fix into a setup sheet or work instruction. Apply it to every station running the same material and tolerance class. A fix that lives in one operator’s head is not a fix.
Step 7: Re-baseline and repeat. Each cycle resets the baseline. Improvement compounds, but only if you keep measuring against the new number.
A worked per-part example. Suppose you cut 10,000 parts per month. Material cost is $2.00 per part. Cutting labor is $0.40 per part. Inspection is $0.10 per part. At a 94% first-pass yield, 600 parts per month need rework at $0.75 each in labor, and 200 of those are scrapped, adding $2.00 each in lost material. That’s $450 in rework labor plus $400 in scrapped material, $850 per month, or $0.085 per part, on top of the base $2.50. Now suppose an accuracy improvement lifts FPY from 94% to 98%. Rework drops to 200 parts ($150) and scrap drops to roughly 70 parts ($140). Monthly loss falls from $850 to $290, a savings of $560 per month, or $0.056 per part, without touching material price, labor rate, or machine speed. Annualized, that’s $6,720 on a single line. Scale that across multiple stations and the case for accuracy investment writes itself.
Where automation fits. Automated cutting systems don’t eliminate this workflow, they make it faster. Calibration checks become software routines. Tool wear can be tracked by cut inches in the controller. Deviation data flows directly into the KPI dashboard. The workflow stays the same; the cycle time between “problem appears” and “problem fixed” shrinks from weeks to hours. That compression is where the compounding savings live.
Frequently Asked Questions
How does cutting accuracy affect production costs?
Cutting accuracy directly influences four cost drivers: material waste, rework labor, production speed, and first-pass yield. When cuts miss tolerances by even 2-3%, manufacturers lose material to scrap, spend hours reworking parts, and slow production throughput. Precision tooling and machine setup quality determine whether your operation achieves these savings.
What is the relationship between material yield and cutting precision?
Material yield is the percentage of raw material that becomes finished product. Cutting precision directly determines yield because inaccurate cuts create scrap, rejects, and parts requiring rework. High-precision cutting yields more material than low-precision cutting. This yield gap translates to significant per-unit cost differences, especially in high-volume production where material cost is the largest expense.
How can manufacturers reduce cutting errors and rework?
Reduce errors through three steps: (1) establish measurable tolerance targets based on design requirements, not guesswork; (2) implement real-time quality control by inspecting first-piece parts and every 50th piece thereafter; (3) use automated cutting systems that eliminate hand-positioning variation and maintain consistent machine setup. Rework reduction comes from catching errors early—inspection at the cut stage costs far less than discovering defects after sewing or assembly. Process optimization workflows that track defect patterns reveal root causes and prevent repeat failures.
Can automated cutting reduce production costs?
Automated cutting systems reduce costs in three ways: lower labor per part through faster throughput, reduced material waste via precision tooling and repeatable setup, and lower rework rates from consistent dimensional accuracy. Automation also improves production speed compared to manual methods, allowing the same crew to handle higher volume. ROI depends on your current waste level, production volume, and material costs.
 EN_US
 ES